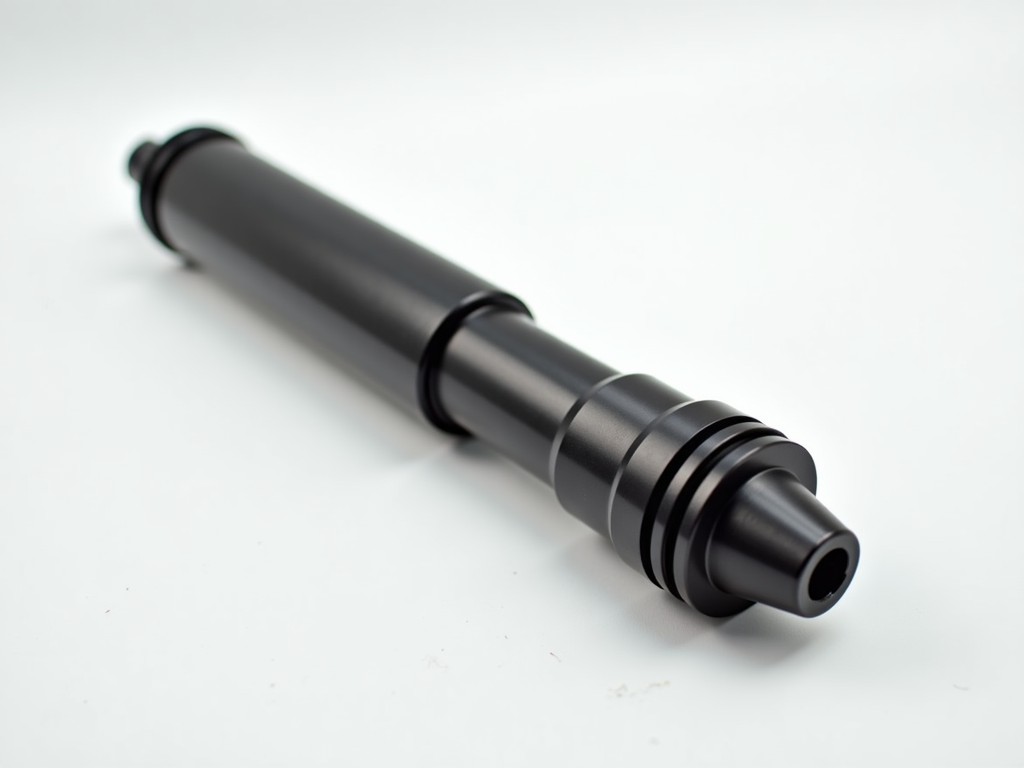
Buy Die Casting Machine Hydraulic Cylinder Injection Nozzle Parts Wholesale
Hydraulic cylinders drive the injection phase of a die‑casting cycle, and the nozzle tip determines metal flow, fill speed, and final part density. Selecting the correct cylinder bore, rod diameter,
Buy Die Casting Machine Hydraulic Cylinder Injection Nozzle Parts Wholesale
Hydraulic cylinders drive the injection phase of a die‑casting cycle, and the nozzle tip determines metal flow, fill speed, and final part density. Selecting the correct cylinder bore, rod diameter, and nozzle geometry reduces cycle time and minimizes porosity in aluminum, magnesium, and zinc alloys.
Wholesale procurement allows OEMs and distributors to standardize spare‑part inventories across multiple press lines. Consistent material grades and heat‑treatment batches lower the risk of dimensional drift between production runs.
Typical Material Options and Their Engineering Rationale
- 42CrMo4 (AISI 4140) quenched & tempered – high tensile strength (≈ 950 MPa) and good wear resistance for cylinder barrels.
- 20CrMnTi carburized – case‑hardened surface (≈ 58 HRC) with a tough core, suited for nozzle tips exposed to molten metal erosion.
- H13 tool steel, nitrided – excellent thermal fatigue resistance, commonly chosen for high‑temperature zinc alloy injection.
- Stainless 17‑4 PH, precipitation hardened – corrosion‑resistant option for machines running water‑based hydraulic fluids.
Material selection is driven by operating pressure (typically 140–210 bar), melt temperature (up to 720 °C for aluminum), and the expected number of cycles before preventive maintenance.
Key Dimensional Parameters
| Parameter | Typical Range | Customization Note |
|---|---|---|
| Cylinder bore | 80 mm – 250 mm | Machined to ±0.02 mm per drawing |
| Rod diameter | 45 mm – 150 mm | Chrome‑plated or nitrided per spec |
| Nozzle tip orifice | 3 mm – 12 mm | Taper angle 15°–30°, polished Ra ≤ 0.4 µm |
| Stroke length | 150 mm – 600 mm | Adjusted to press platen spacing |
| Maximum working pressure | 210 bar | Design safety factor 4:1 |
Why These Parts Fit High‑Volume Die‑Casting Lines
A precise bore‑to‑rod clearance maintains consistent hydraulic damping, which directly controls injection velocity profiles. When the nozzle tip geometry matches the runner system, turbulence is reduced, lowering the incidence of cold‑shut defects.
Heat‑treated barrels resist scoring from high‑speed rod motion, extending service intervals from 30 k to 80 k cycles in typical aluminum casting cells. Carburized nozzle tips retain hardness after repeated exposure to molten metal, decreasing replacement frequency and unplanned downtime.
Customization Workflow for Wholesale Orders
- Submit 2D/3D drawings or OEM part numbers.
- Engineering review confirms material, heat‑treatment, and coating requirements.
- Prototype batch (typically 5–10 pcs) produced for first‑article inspection.
- Full‑scale production scheduled after dimensional and hardness sign‑off.
- Batch traceability records (material certs, heat‑treat logs) shipped with each lot.
Lead time for a standard catalog item is 3–4 weeks; custom geometries add 1–2 weeks for tooling preparation.
Quality Assurance and Inspection Standards
- Dimensional inspection per ISO 286‑2 using CMM (±0.01 mm on critical diameters).
- Hardness verification (Rockwell C or Vickers) on each heat‑treat lot.
- Surface roughness measurement on nozzle tips (Ra ≤ 0.4 µm).
- Hydrostatic pressure test at 1.5× rated pressure for 30 minutes.
- Material certification (EN 10204 3.1) supplied with every shipment.
Packaging and Export Protection
Cylinders are individually wrapped in VCI‑impregnated film, placed in wooden crates with foam inserts, and secured with steel strapping. Nozzle tips receive additional anti‑corrosion oil coating and are packed in sealed poly‑bags to prevent moisture ingress during sea freight.
Frequently Asked Questions
- Can the bore and rod dimensions be customized?
- Yes. Provide the target bore, rod, and stroke; we machine to ±0.02 mm tolerance per your drawing.
- What information is needed for a quotation?
- Part drawing or OEM number, material grade, heat‑treatment spec, surface coating, quantity, and desired delivery schedule.
- Which materials are available for nozzle tips?
- 20CrMnTi carburized, H13 nitrided, 17‑4 PH, and other tool steels on request.
- How is quality inspected before shipment?
- Full CMM dimensional check, hardness test, surface roughness, hydrostatic pressure test, and material cert review.
- What packaging options exist for export?
- Standard VCI‑wrapped crates, optional fumigated pallets, and custom labeling per customer requirement.
- Typical production lead time for a wholesale batch?
- 3–4 weeks for catalog items; 4–6 weeks for custom geometries including first‑article approval.
Next Steps
Ready to align spare‑part inventory with your press specifications? Request a detailed quotation and receive a material‑certification package for review.
For technical datasheets or to discuss a prototype run, contact our engineering team directly.