
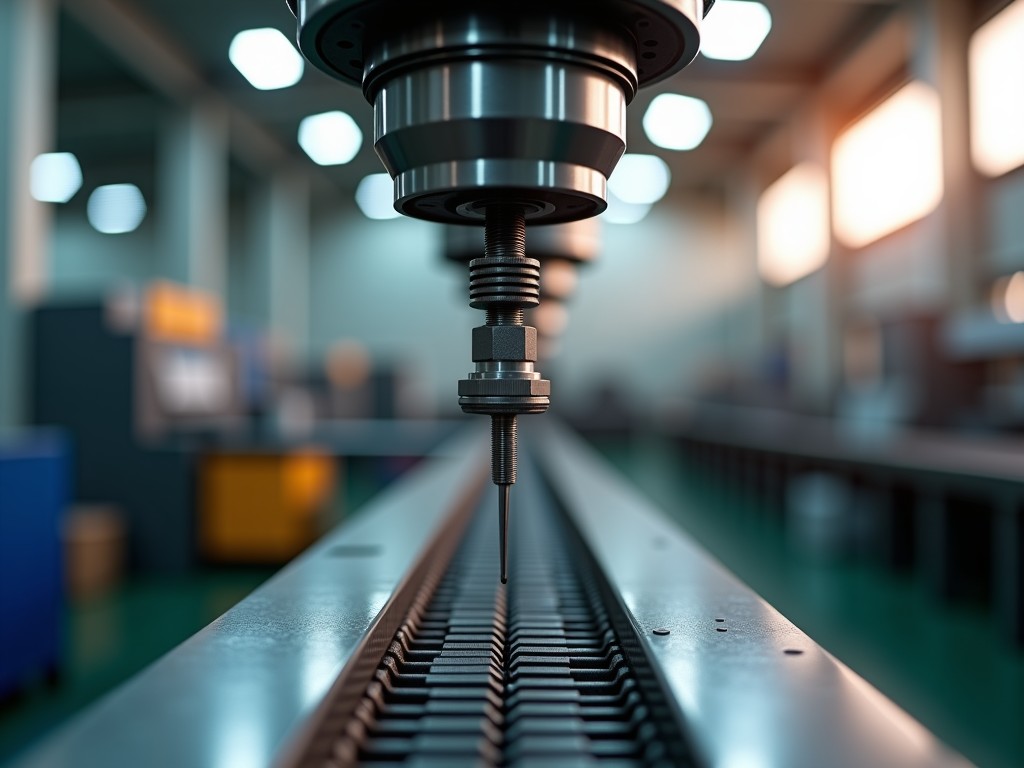
Oem Metal Zipper Tooth Making Machine Top Factory
Manufacturers of metal zipper components require equipment that delivers consistent tooth geometry at high throughput while accommodating a range of alloys and surface finishes. This page outlines
OEM Metal Zipper Tooth Making Machine – Top Factory Solutions
Manufacturers of metal zipper components require equipment that delivers consistent tooth geometry at high throughput while accommodating a range of alloys and surface finishes. This page outlines the engineering basis, standard specifications, and customization pathways for the machines most commonly supplied to OEM zipper producers.
Core Design Philosophy
The machine architecture centers on a modular die‑set that can be swapped without removing the main drive, reducing change‑over time from hours to under 30 minutes. A servo‑driven feed system synchronizes strip advancement with the stamping cycle, eliminating the pitch variation that plagues cam‑driven legacy units.
Thermal management is handled by a closed‑loop coolant circuit that maintains the die temperature within ±2 °C, a critical factor when forming high‑strength brass or stainless‑steel alloys that work‑harden rapidly.
Technical Specifications (Typical Values)
| Parameter | Typical Range | Notes |
|---|---|---|
| Model | ZTM‑300 / ZTM‑500 / ZTM‑800 | Scalable by adding parallel stamping stations |
| Production Speed | 120 – 350 teeth/min per station | Adjustable via servo profile |
| Tooth Pitch Range | 2.0 – 5.5 mm | Custom pitches available on request |
| Material Compatibility | Brass, copper‑nickel, stainless steel 304/316, aluminum alloys | Die coating selected per alloy |
| Power Consumption | 7.5 – 15 kW (three‑phase 380 V) | Includes coolant pump and servo drives |
| Overall Dimensions (L×W×H) | 2,200 × 1,100 × 1,850 mm | Footprint grows with added stations |
| Machine Weight | 3,200 – 5,800 kg | Depends on configuration |
| Control System | PLC + HMI (Siemens/Allen‑Bradley compatible) | Remote diagnostics via Ethernet |
Key Functional Modules
- Servo‑driven strip feed with closed‑loop encoder feedback for sub‑micron positioning.
- Quick‑change die cassette using hydraulic locking pins; no tools required.
- Integrated lubrication mist system that applies a measured film to each tooth, reducing galling on stainless grades.
- Real‑time force monitoring on each stamping station; out‑of‑tolerance events trigger automatic stop and data logging.
Why This Machine Fits Zipper OEM Production
Zipper tooth geometry directly influences slider engagement force and fatigue life. The servo‑controlled pitch ensures that each tooth meets the ±0.02 mm tolerance required for high‑cycle slider testing, a level difficult to achieve with mechanical cam drives.
The coolant‑stabilized die temperature prevents micro‑cracking in work‑hardened stainless steel, extending die life from an average of 1.2 million strokes to over 2.5 million strokes under typical OEM volumes.
Modular station addition lets a line scale from a single‑head prototype cell to a 12‑head high‑volume line without redesigning the base frame, protecting capital investment as demand grows.
Customization Options
Every OEM project begins with a specification review. The following variables are routinely tailored:
- Tooth profile geometry (standard Y‑type, reverse‑Y, flat‑top, or proprietary shapes).
- Die coating selection: TiN, CrN, DLC, or uncoated for soft alloys.
- Strip width and thickness range (0.3 – 1.2 mm, 8 – 30 mm wide).
- Integration of inline vision inspection for tooth height and symmetry.
- Automation interfaces: robot load/unload, conveyor sync, MES data exchange.
Quality Assurance & Inspection
Each machine undergoes a factory acceptance test (FAT) that includes:
- Dimensional verification of 500 consecutive teeth using a calibrated optical comparator.
- Force‑stroke curve recording at nominal and maximum speed.
- Thermal stability run of 8 hours with continuous coolant temperature logging.
- Electrical safety compliance to IEC 60204‑1 (CE marked on request).
Statistical process control (SPC) data packets are shipped with the equipment, enabling the buyer to continue monitoring key parameters from day one.
Packaging, Shipping & Installation Support
Machines are disassembled into major sub‑assemblies (frame, drive module, die cassette, control cabinet) and secured in fumigated wooden crates with shock‑absorbing foam. Standard export packaging complies with ISPM‑15.
On‑site commissioning includes mechanical alignment, servo tuning, and a 40‑hour production validation run. Remote support is available for 12 months via the HMI VPN link.
Frequently Asked Questions
- Can the tooth pitch be changed after installation? Yes – the servo profile stores multiple pitch recipes; switching takes < 2 minutes via the HMI.
- What information is needed for a quotation? Strip material, thickness, width, desired tooth profile, target output (teeth/min), and any required automation interfaces.
- Are spare die sets available? Standard die sets are stocked for the most common pitches; custom dies are manufactured to order with a 4‑week lead time.
- How is machine accuracy verified over time? Built‑in force and position sensors feed SPC charts; periodic calibration kits are supplied.
- What are the typical lead times? 8‑10 weeks for a standard 3‑station configuration; additional stations add 2‑3 weeks each.
- Is operator training included? A two‑day on‑site training session is standard; supplementary e‑learning modules are provided.
Next Steps
To discuss your specific zipper tooth requirements, request a detailed specification sheet, or schedule a virtual line audit, please reach out through our contact form.
Request a Quotation


